Understand your requirement
Review part, product and process variation for robotic loading of production fixtures, arrival pattern and presentation, and required cycle and production pattern using your samples, drawings and production observations.
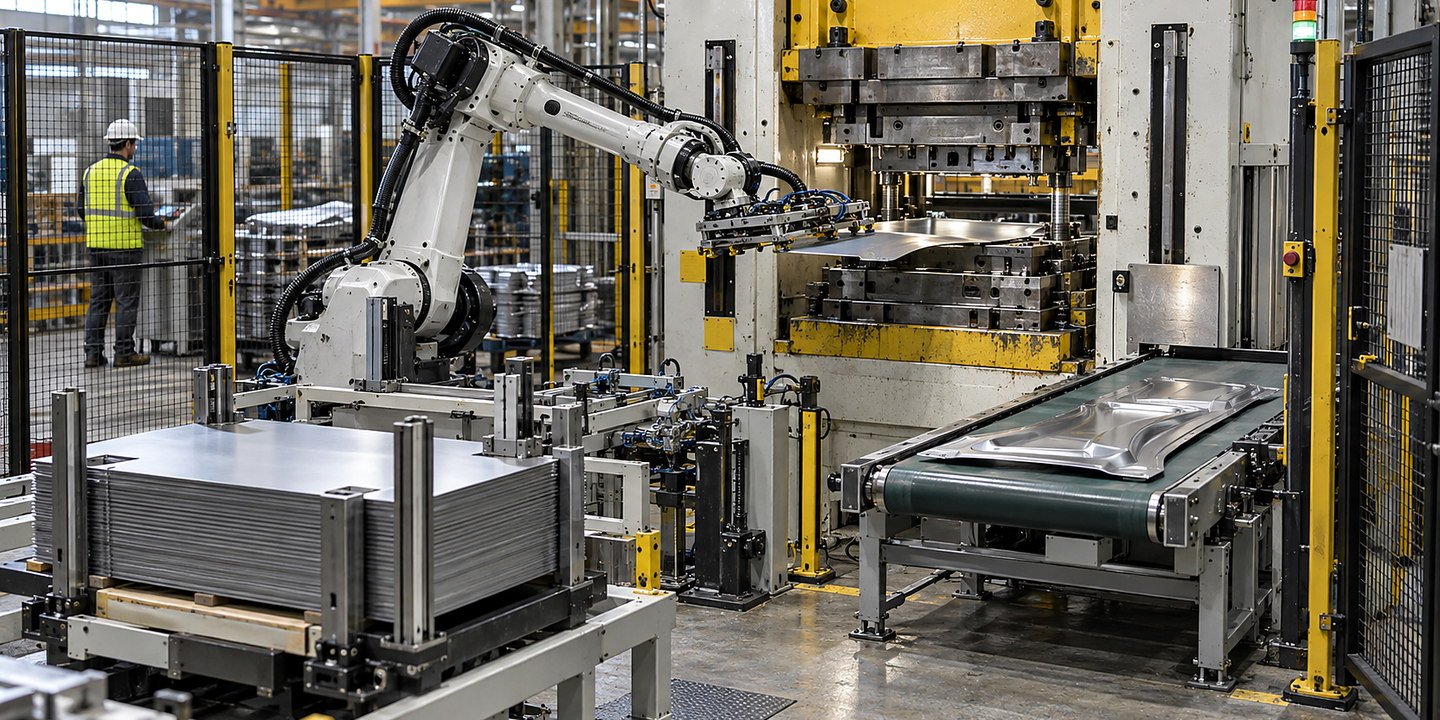
Compare practical options for robotic loading of production fixtures, including what each route needs, where it fits and what to check before you decide.
The right solution for robotic fixture loading is the simplest system that reliably handles your stated duty, line connections and expected exceptions.
Plan robotic fixture loading around your parts, process, cycle time, tooling, recovery and acceptance criteria. Discuss the highest-risk feasibility questions with Oxford Industrial Automation.
Plan robotic fixture loading around your parts, process, cycle time, tooling, recovery and acceptance criteria. Discuss the highest-risk feasibility questions with Oxford Industrial Automation. When you compare solutions, check how each option handles part, product and process variation for robotic loading of production fixtures, arrival pattern and presentation and your surrounding line.
Discuss your application

Review part, product and process variation for robotic loading of production fixtures, arrival pattern and presentation, and required cycle and production pattern using your samples, drawings and production observations.
Run focused trials for robotic fixture loading so you can see why an option is recommended or ruled out.
Resolve tooling, sensing and process interfaces, operator access, recovery and changeover, controls, safety, operator access and maintenance before site work.
Check run-off criteria and production evidence in normal, difficult and fault conditions, then agree training and support for your team.
Typical support: feasibility study, sample trials, cell design, offline build, integration and production ramp-up.
| Approach | Often suitable when | Watch for |
|---|---|---|
| Robotic Fixture Loading | You need a dedicated solution for a clearly defined duty, product or part range and line interface. | Cycle time depends on the complete process rather than robot speed alone. |
| Purpose-Built Mechanical Automation for a Stable, Very High-Volume Task | The part and fixture range, loading sequence and production pattern are stable enough to investigate a dedicated mechanism. | Assess approach, seating, release, dimensional variation and confirmation of correct location, including the effect of future part or fixture changes. |
| Operator-Assisted Fixtures where Flexibility or Business Case Does Not Support a Robot Cell | Variant changes, manual presentation or operator judgement make an assisted fixture worth comparing with a robot cell. | Define operator tasks, access, the location check and the response to an uncertain loaded condition, then compare the complete cycle. |