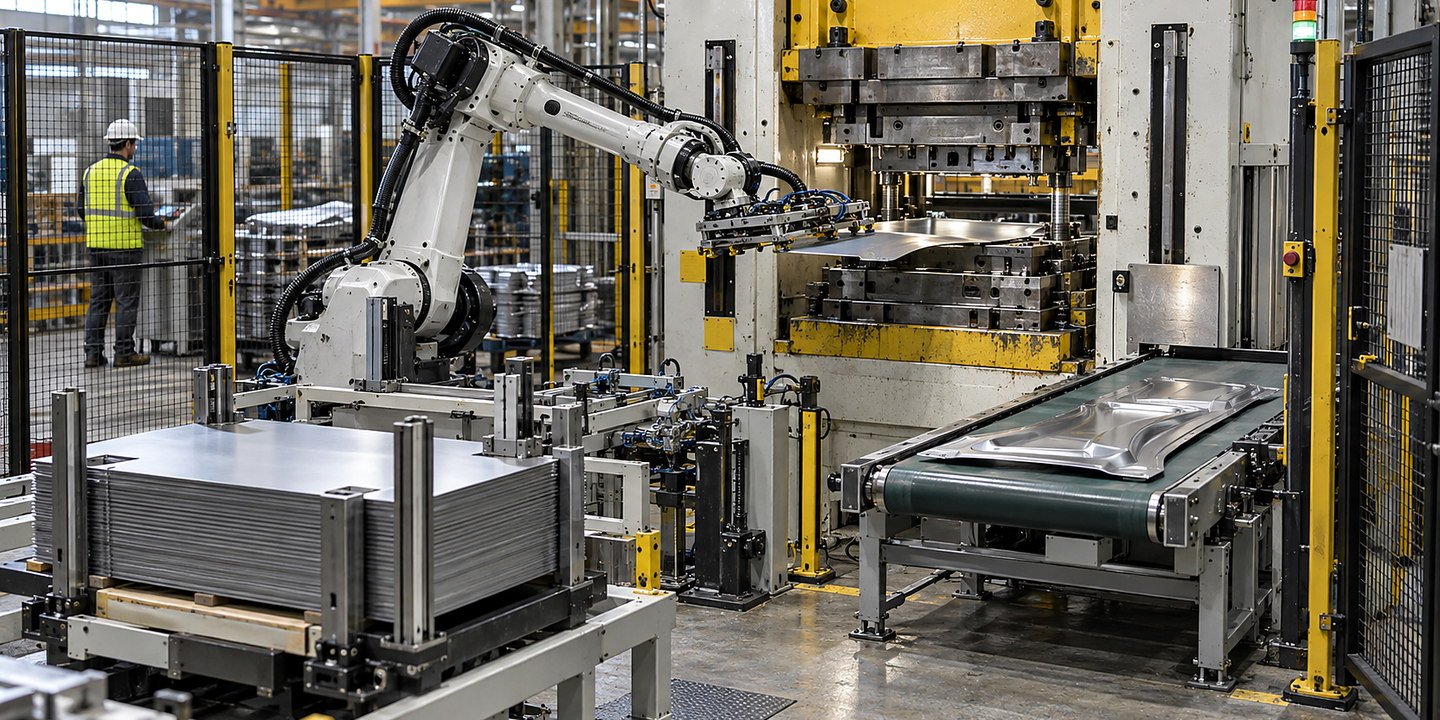
Plan mechanical, electrical, control, data, safety and operator interfaces for robotic fixture loading.
In brief
Fixture-loading integration must connect the part arrival condition, fixture availability, required loaded location and permission for the next process. Define the physical interfaces and the information needed at each hand-off before choosing a control method.
For each state, identify who supplies it, what confirms it and what happens when it is absent or uncertain. Carry these requirements into the complete-line acceptance checks.
On the production floor
Connect equipment, controls and people into one reliable process — Robotic Fixture Loading
Plan robotic fixture loading around your parts, process, cycle time, tooling, recovery and acceptance criteria. Discuss the highest-risk feasibility questions with Oxford Industrial Automation. Your integration review should connect required cycle and production pattern, tooling, sensing and process interfaces and the people who run the process.
Six areas to coordinate for robotic fixture loading
Mechanical
Provide the part and fixture location features, proposed tooling and the space needed for approach, seating and release. Review the interfaces, access and known dimensional variation together; record constraints requiring further assessment.
Electrical
For Robotic Fixture Loading, list the supplies, isolation, protective devices, panels and cable routes required by the proposed installation.
Controls
Agree the required states for part availability, fixture readiness, loading, location confirmation and next-process permission. Define the response to missing or conflicting information and the checks required before resumption.
Safety
Review risk controls, stop behaviour, access, reset and the checks needed around tooling, sensing and process interfaces.
Data
Agree whether part and fixture revision, selected variant, location-check result and exception records are required. Define each record, its source, reviewer and retention needs without assuming a particular data system.
Your team
Assign responsibility for replenishment, fixture changeover, review of uncertain loading and checks before restart. Include cleaning, maintenance, training and access requirements for the actual part and fixture range.
How the work comes together
Plan fault recovery for loading production fixtures with a robot as carefully as normal running
For Robotic Fixture Loading, your team can review each stage before the complete installation is put into routine use.
01
Observe the Current Process and Collect Representative Samples
Share representative parts, process observations and cycle data, including the normal range for part, product and process variation for robotic loading of production fixtures and the difficult arrival pattern and presentation cases.
02
Prove Handling and Process Risks in a Focused Feasibility Trial
Compare suitable methods and use focused trials to show how each option performs against required cycle and production pattern.
03
Design and Build the Complete Guarded Cell
Connect the equipment to your line, services and controls while resolving tooling, sensing and process interfaces for day-to-day operation.
04
Run Agreed Scenarios and Support Production Ramp-Up
Confirm operator access, recovery and changeover, then complete and record run-off criteria and production evidence before your operating team takes over.
For your application: check required cycle and production pattern, tooling, sensing and process interfaces, operator access, recovery and changeover, and run-off criteria and production evidence as part of the complete line trial.
Important limits
Line connections can change the approach for Robotic Fixture Loading
Cycle time depends on the complete process rather than robot speed alone.
Part presentation, tolerances and recovery cases must be included in feasibility work.
Collaborative operation or automatic handling cannot be assumed safe without an application assessment.