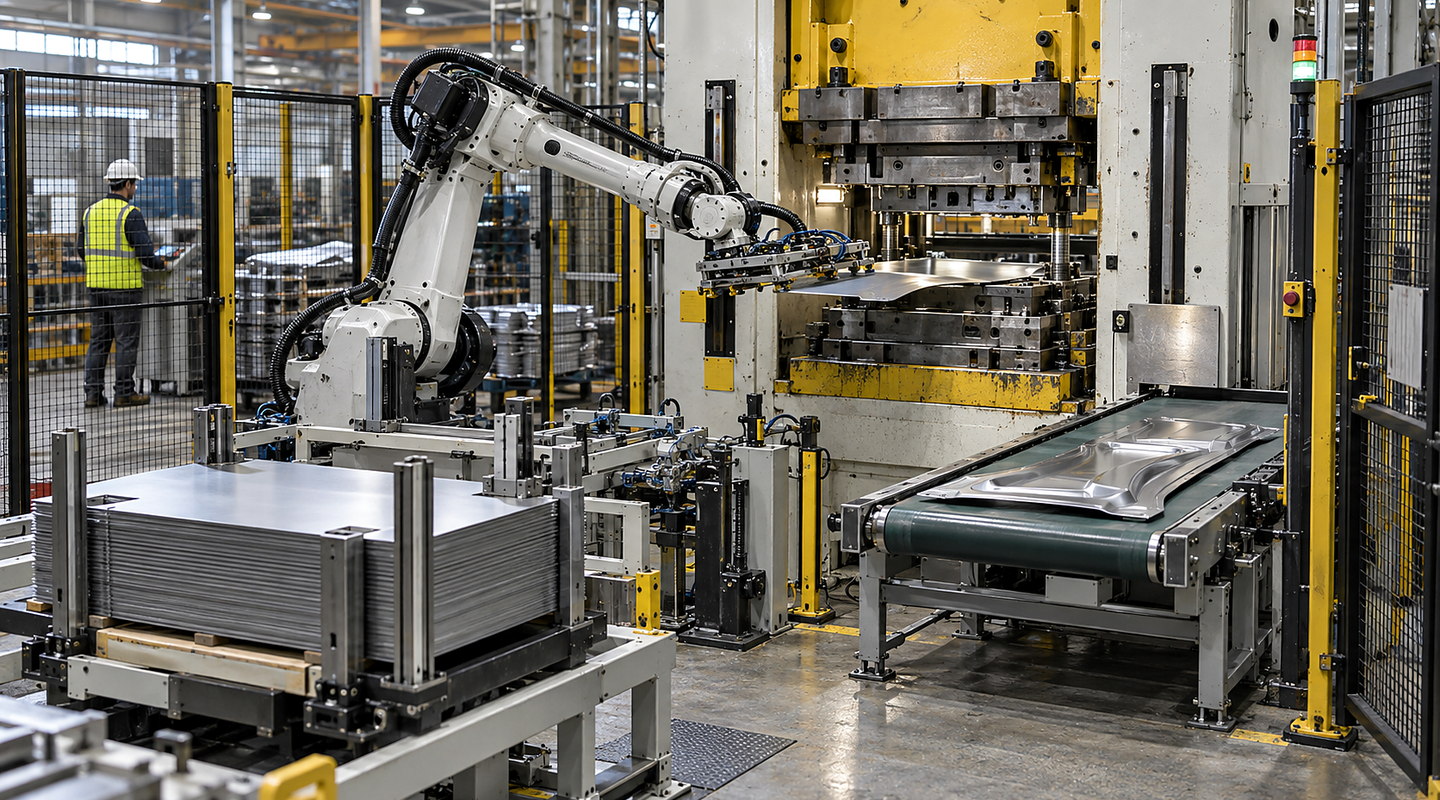
Flexible Fixture Loading Across Multiple Part Variants
Plan flexible fixture loading across multiple part variants around representative parts, tooling and the complete process sequence, line connections, operating limits, acceptance checks and next steps.
In brief
For multiple part variants, define each part and fixture combination, its drawing revision, location features and allowed condition at loading. Compare the approach, seating, release and location checks required for each combination before assuming one arrangement can handle them all.
Use the variation guide to choose representative combinations. Record which changes require different tooling, fixture arrangements or settings as questions for assessment, not established flexibility.
On the production floor
Plan for the conditions your team handles every day — Robotic Fixture Loading
Plan robotic fixture loading around your parts, process, cycle time, tooling, recovery and acceptance criteria. Discuss the highest-risk feasibility questions with Oxford Industrial Automation. For flexible fixture loading across multiple part variants, the deciding details include part, product and process variation for robotic loading of production fixtures, required cycle and production pattern and run-off criteria and production evidence.
Details worth resolving early for flexible fixture loading across multiple part variants
Question 1
Part, Product and Process Variation for Robotic Loading of Production Fixtures
List the intended part and fixture combinations, revisions and location features. Define the accepted loaded condition for each and identify differences that could affect approach, seating or release.
Question 2
Arrival Pattern and Presentation
Describe how each variant arrives and the orientation required at its fixture. Include presentation differences and dimensional variation in the assessment instead of relying on one convenient sample.
Question 3
Required Cycle and Production Pattern
State the variant mix, batch pattern and required complete cycle. Include replenishment, location checks, line waits and variant changeover where they apply; keep observed times separate from targets.
Question 4
Tooling, Sensing and Process Interfaces
Identify proposed tooling and fixture arrangements and the settings or interfaces that may change between variants. Agree how the selected part and fixture combination and its required location will be confirmed before the next process.
Question 5
Operator Access, Recovery and Changeover
Define the changeover tasks, responsible people and checks before the first part of a new variant. Include the response to an obstructed fixture, missing part or incomplete seating; do not assume automatic correction.
Question 6
Run-Off Criteria and Production Evidence
Agree which part and fixture combinations represent the intended range, the assessed method and repetitions, and the acceptable loaded condition. Record the combinations examined, unresolved cases and limits for future variants.
Your operating cycle
Plan for more than automatic running
Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for flexible fixture loading across multiple part variants. A fast automatic step can still leave your team with a slow or awkward overall process.
Normal production and variant changes
Replenishment and material presentation
Operator access and safe interventions
Cleaning, maintenance and recovery
Prove the result
Test flexible fixture loading across multiple part variants against representative parts, tooling and difficult cycle conditions
Normal production
Run the agreed product or part mix for flexible fixture loading across multiple part variants at your intended operating pattern.
Difficult conditions
Include credible extremes for part, product and process variation for robotic loading of production fixtures and arrival pattern and presentation.
Fault and recovery
Agree an assessed method for reviewing credible part and fixture mismatches, obstruction, missing parts or incomplete seating. Define the required indication, hold and review route and the conditions for resumption; detection and recovery methods remain to be established.
Important limits
Be clear about what the trial has shown
Cycle time depends on the complete process rather than robot speed alone.
Part presentation, tolerances and recovery cases must be included in feasibility work.
Collaborative operation or automatic handling cannot be assumed safe without an application assessment.